Pipe fittings
Butt weld tees, reducers, caps, crosses and stub ends
The full family of wrought butt weld fittings - equal and reducing tees, concentric and eccentric reducers, caps, crosses and lap joint stub ends - to ASME B16.9 and MSS SP-43.
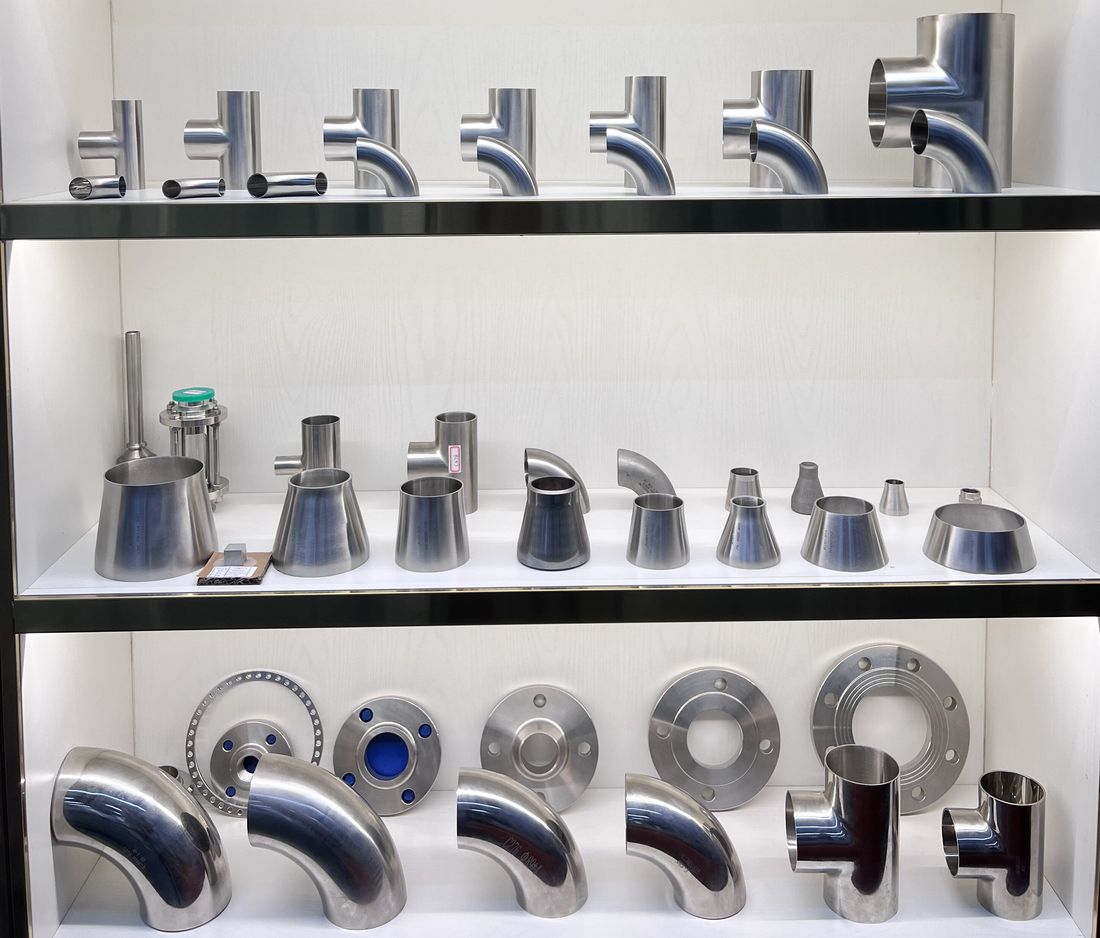
Dimensions and reference data
| Fitting | Size range | Wall thickness | Forming route |
|---|---|---|---|
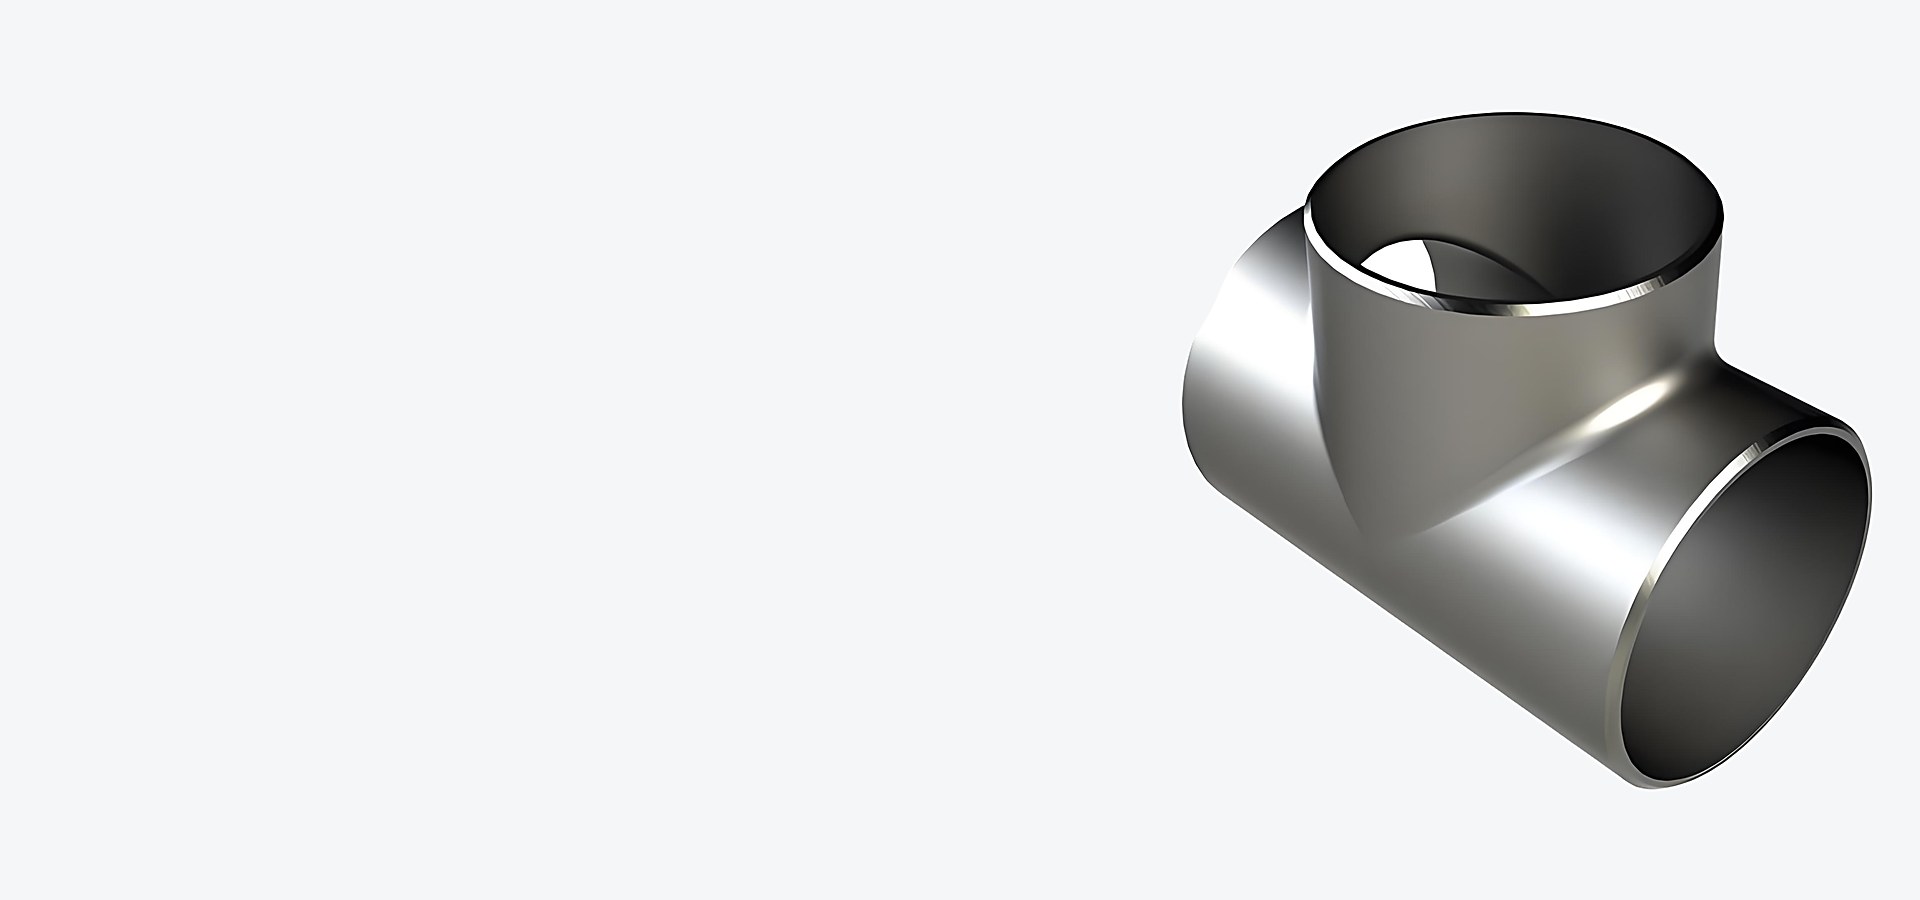
| Straight / equal tee | NPS ½ – 48 | Schedule 5S – XXS | Extruded outlet from seamless pipe or hot pressed plate |
| Reducing tee | NPS ½ – 48 | Schedule 10S – XXS | Extruded outlet then contoured to the reduced branch size |
| Barred tee | NPS 4 – 48 | Schedule 40S – XXS | Carbon or alloy steel bar cage welded inside for pigging duty |
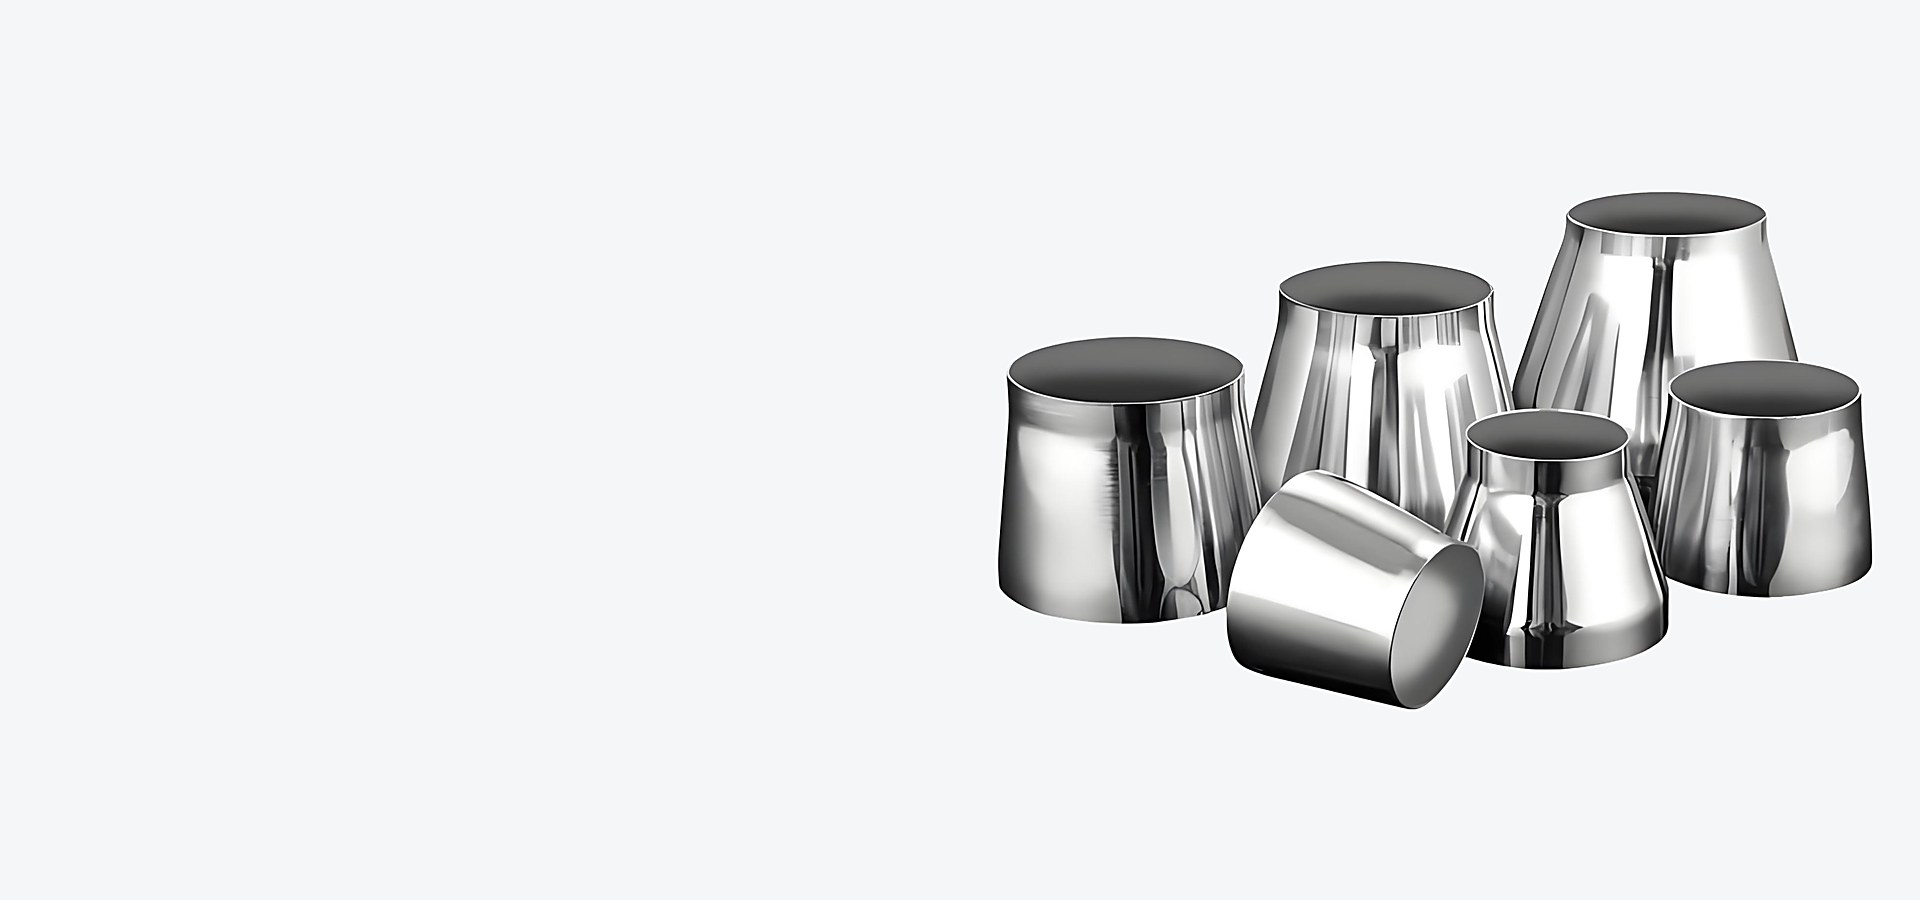
| Concentric reducer | NPS ¾ – 48 | Schedule 10S – XXS | Pressed and welded from plate, or turned from solid for heavy walls |
View all 8 rows
| Fitting | Size range | Wall thickness | Forming route |
|---|---|---|---|
| Eccentric reducer | NPS ¾ – 48 | Schedule 10S – XXS | Pressed and welded from plate with one face flat |
| Cap | NPS ½ – 48 | Schedule 10S – XXS | Deep drawn or pressed from plate with a full penetration cap weld where required |
| Stub end, long pattern | NPS ½ – 24 | Schedule 10S – 160 | Machined from pipe or bar to ASME B16.9 dimensions |
| Stub end, short pattern | NPS ½ – 24 | Schedule 5S – 10S | MSS SP-43 light wall for low pressure systems |
Larger sizes and heavy wall combinations are frequently welded from plate with 100 % radiography of the longitudinal seam before forming; this route is disclosed on the quotation.
| Grade family | Material specification | Typical applications | Wire / filler |
|---|---|---|---|
| Inconel 625 | ASTM B366 WP625 Gr.1 or Gr.2 | Seawater, sour service, FGD | ERNiCrMo-3 |
| Incoloy 825 | ASTM B366 WP825 | Sulphuric acid, produced water | ERNiFeCr-1 |
| Hastelloy C-276 | ASTM B366 WPHC276 | Reactors, scrubbers, mixed acid | ERNiCrMo-4 |
| Monel 400 | ASTM B366 WP400 | HF alkylation, marine systems | ERNiCu-7 |
| Titanium Grade 2 / 5 | ASTM B363 WPT2 / WPT5 | Desalination, chlorine, offshore | ERTi-2 / ERTi-5 |
| Duplex 2205 / 2507 | ASTM A815 WP-S / WP-W | Subsea, brine, firewater | ER2209 / ER2594 |
| 316L / 321 / 347 | ASTM A403 WP316L / WP321 / WP347 | General process and hygienic lines | ER316L / ER347 |
Specifications and options
| Dimensional standard | ASME B16.9; MSS SP-43 for light wall Schedule 5S and 10S |
|---|---|
| Branch outlets | MSS SP-97 weldolets, sockolets, threadolets, elbolets and latrolets machined from solid bar |
| Nickel alloys | ASTM B366 / ASME SB-366 in Inconel, Incoloy, Hastelloy, Monel and nickel grades |
| Titanium | ASTM B363 / ASME SB-363 WPT2, WPT5, WPT7, WPT12 |
| Stainless & duplex | ASTM A403 WP316L, WP321, WP347, WP904L, WPS31254 and ASTM A815 duplex grades |
| End preparation | ASME B16.25 bevelled ends for butt welding; square cut for socket weld products |
| Heat treatment | Solution anneal with recorded furnace charts and 'as treated' mechanical tests per heat lot |
| NDT | DPT on formed zones, RT on all plate-formed seams, UT and PMI available as specified |
| Marking | Manufacturer, grade, schedule, size and heat number stencilled or etched |
| Certification | EN 10204 3.1; SGS third party test report available |
Typical applications
- Branch take-offs on chemical and petrochemical process headers
- Pump suction and discharge transitions requiring concentric or eccentric reducers
- Line terminations and future extension points using caps with removable insulation covers
- Lap joint flange assemblies for lines requiring frequent stripping and cleaning
- Barred tees on multiphase pipelines that require intelligent pigging
- Instrument and sampling connections using MSS SP-97 branch outlets
- Skid packages where multiple diameter changes must fit inside a tight footprint
How to order pipe fittings – tees, reducers, caps & stub ends
Send us the following and we will return a quotation within 24 hours: alloy grade or UNS number, dimensions including schedule or wall thickness, governing material and dimensional standards, quantity, required heat treatment, non-destructive testing scope, certificate type and any third party inspection requirement.
Pipe Fittings – Tees, Reducers, Caps & Stub Ends frequently asked questions
When should I use an eccentric reducer?
Use an eccentric reducer on horizontal pump suction lines with the flat side installed up, so that vapour cannot accumulate at the top of the line and cause cavitation. Concentric reducers suit vertical lines and stacked pump suction.
What is a barred tee and when is it needed?
A barred tee has internal bars welded across the run so that a pig cannot enter the branch. They are mandatory on piggable multiphase and subsea pipelines where the branch line connects to a small bore service.
Are your tees seamless?
Up to roughly NPS 16 most nickel alloy tees can be produced from seamless pipe with an extruded outlet. Above that, or for very heavy walls, tees are pressed from plate with a fully radiographed seam - details are always declared before order.
What is the difference between ASME B16.9 and MSS SP-43 fittings?
MSS SP-43 covers light wall corrosion resistant fittings in Schedule 5S and 10S and has looser tolerances and lower cost. ASME B16.9 covers the full wall thickness range and is required for code pressure piping.
Can you produce reinforcing outlets such as weldolets?
Yes. Branch outlets to MSS SP-97 are machined from solid bar in the same alloy as the header, which avoids the dilution and heat affected zone problems of a fabricated branch weld.
Do you size stub ends to match your lap joint flanges?
Yes. We machine stub ends to ASME B16.9 Type A dimensions for use with ASME B16.5 lap joint flanges, with the lap face machined flat and radiused to prevent stress concentration.