Pipe fittings
Butt weld elbows in nickel alloys, titanium and special stainless steel
Hangbo manufactures butt weld elbows to ASME B16.9 dimensions (and MSS SP-43 for light wall) in Inconel, Hastelloy, Monel, Incoloy, titanium and duplex stainless steel, from NPS ½ to NPS 48.
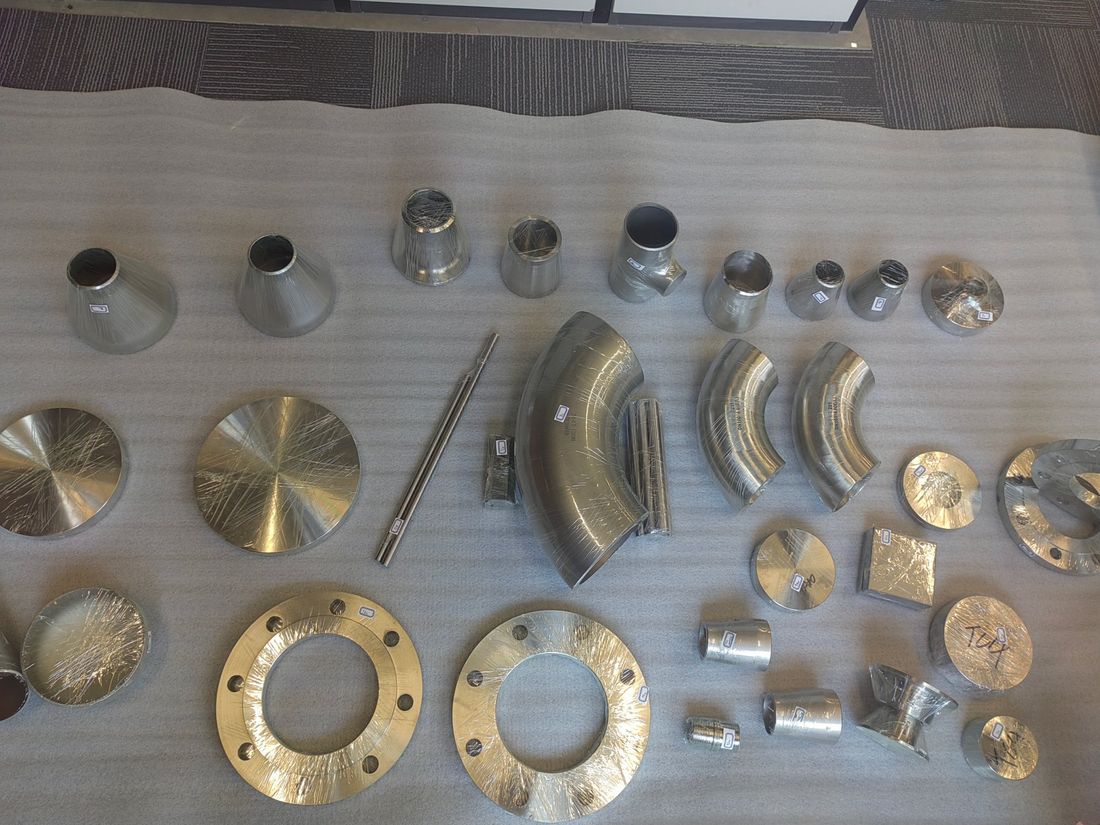
Dimensions and reference data
| NPS | DN | Outside diameter (mm) | 90° LR centre-to-end A (mm) | 90° SR centre-to-end A (mm) |
|---|---|---|---|---|
| ½ | 15 | 21.3 | 38 | – |
| ¾ | 20 | 26.7 | 38 | – |
| 1 | 25 | 33.4 | 38 | 25 |
| 1½ | 40 | 48.3 | 57 | 38 |
View all 14 rows
| NPS | DN | Outside diameter (mm) | 90° LR centre-to-end A (mm) | 90° SR centre-to-end A (mm) |
|---|---|---|---|---|
| 2 | 50 | 60.3 | 76 | 51 |
| 3 | 80 | 88.9 | 114 | 76 |
| 4 | 100 | 114.3 | 152 | 102 |
| 6 | 150 | 168.3 | 229 | 152 |
| 8 | 200 | 219.1 | 305 | 203 |
| 10 | 250 | 273.0 | 381 | 254 |
| 12 | 300 | 323.9 | 457 | 305 |
| 16 | 400 | 406.4 | 610 | 406 |
| 20 | 500 | 508.0 | 762 | 508 |
| 24 | 600 | 609.6 | 914 | 610 |
Long radius centre-to-end A equals 1.5 x NPS in inches converted to millimetres; short radius equals 1.0 x NPS. The 45° long radius centre-to-end dimension B is approximately 0.414 x A, for example 64 mm for NPS 4 and 189 mm for NPS 12. Full tables covering every NPS size are issued with each quotation or on request.
| NPS range | DN range | O.D. at bevel (mm) | I.D. at end (mm) | Off angle Q (mm) | Off plane P (mm) |
|---|---|---|---|---|---|
| ½ – 2½ | 15 – 65 | +1.6 / -0.8 | ±0.8 | ±1 | ±2 |
| 3 – 3½ | 80 – 90 | ±1.6 | ±1.6 | ±2 | ±4 |
| 4 | 100 | ±1.6 | ±1.6 | ±3 | ±5 |
| 5 – 8 | 125 – 200 | +2.4 / -1.6 | ±1.6 | ±3 | ±6 |
| 10 – 18 | 250 – 450 | +4.0 / -3.2 | ±3.2 | ±4 | ±10 |
| 20 – 24 | 500 – 600 | +6.4 / -4.8 | ±4.8 | ±5 | ±10 |
| 26 – 30 | 650 – 750 | +6.4 / -4.8 | ±4.8 | ±5 | ±13 |
| 32 – 48 | 800 – 1200 | +6.4 / -4.8 | ±4.8 | ±5 | ±19 |
Specifications and options
| Dimensional standard | ASME B16.9 (factory-made wrought butt welding fittings); MSS SP-43 for light wall |
|---|---|
| Nickel alloy material | ASTM B366 / ASME SB-366 - WP625, WP718, WPHC276, WPHC22, WP400, WP500, WP825, WP800H / WP800HT, WP600, WP601, WPX |
| Titanium material | ASTM B363 / ASME SB-363 - WPT2, WPT5, WPT7, WPT12 |
| Duplex / stainless material | ASTM A815 (WP-S32205, WP-S32750), ASTM A403 (WP316L, WP321, WP347, WP904L, WPS31254) |
| Seamless pipe feedstock | ASTM B444, B423, B622, B167, B861, A312, A790 depending on grade |
| End preparation | ASME B16.25 butt welding ends, 37.5° ± 2.5° bevel unless specified otherwise |
| Heat treatment | Solution anneal and quench per the applicable material specification, recorded per heat lot |
| NDT | Dye penetrant on all formed areas; radiographic or ultrasonic testing to order |
| Marking | Manufacturer symbol, material grade, wall thickness designation, size and heat number |
| Certification | EN 10204 3.1 with chemical analysis, mechanical properties, heat treatment record and dimensions |
Typical applications
- Chemical process pipework carrying mixed acids, solvents and chlorinated streams
- Offshore seawater lift, firewater, cooling water and produced water lines
- Refinery heater outlet pigtails, transfer lines and hydrocracker circuits
- Flue gas desulphurisation absorber recirculation and slurry lines
- Power station feedwater, condensate and flue gas duct transitions
- LNG and cryogenic transfer lines where low temperature toughness is required
- Piggable long radius bend systems for subsea and cross-country pipelines
How to order butt weld elbows
Send us the following and we will return a quotation within 24 hours: alloy grade or UNS number, dimensions including schedule or wall thickness, governing material and dimensional standards, quantity, required heat treatment, non-destructive testing scope, certificate type and any third party inspection requirement.